Enclosed Dust-Tight Separation: Protecting Cleanroom Air Quality in Linear Protein Powder Screening
Post Date: 2026-10-24
In large-scale protein powder manufacturing—where high-capacity streams of whey, soy, pea, or rice protein flow through high-volume screening decks—managing airborne dust emissions is critical to operational success. Fine protein particles possess low bulk density and readily aerosolize under high-frequency linear vibration. Uncontained powder dust degrades cleanroom air quality, increases risk of cross-contamination, overburdens facility HVAC systems, and compromises workplace safety.
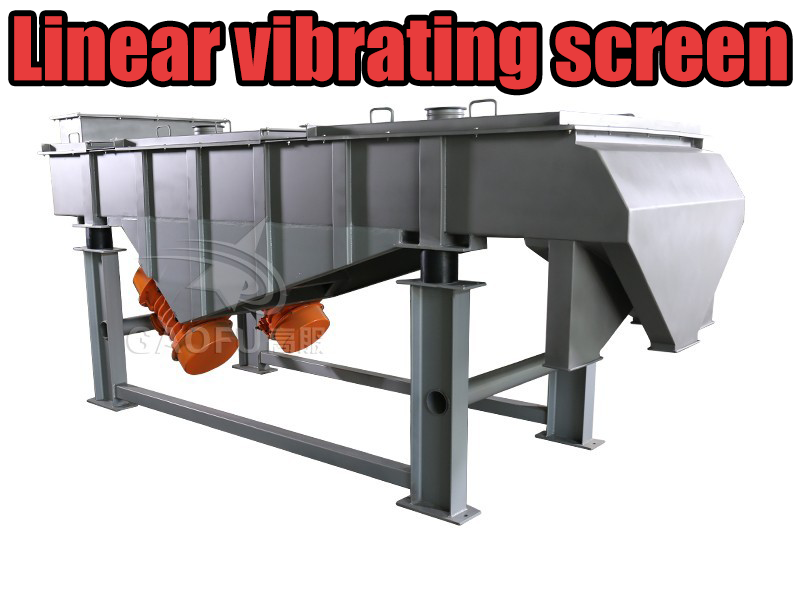
At Gaofu Machinery, we combine bulk linear separation performance with advanced dust-containment engineering. Our Linear Vibrating Screen features a fully enclosed, dust-tight design built to protect cleanroom environments while maintaining continuous high-volume throughput.
Understanding the Airborne Dust Challenge in Linear Screening
Linear vibrating screens utilize dual counter-rotating motors to propel high volumes of powder across long rectangular screen decks in continuous parabolic arcs. While highly efficient for bulk classification and scalping, this dynamic movement creates internal air agitation within the screen box:
- HVAC Filter Overloading: Unsealed screening boxes release airborne particulates into ambient room air, clogging HEPA filters prematurely and throwing off cleanroom static pressure balances.
- Batch Cross-Contamination: Suspended fine powders settle on nearby structural steel, conveyor lines, and neighboring processing stations, creating allergen control challenges during multi-product runs.
- Combustible Dust & Workplace Safety: High concentrations of airborne organic dust present combustible dust hazards and respiratory burdens for operators, requiring constant ambient monitoring and heavy PPE.
Core Dust-Mitigation Innovations in Gaofu’s Linear Screen
Our linear screening box is engineered from the ground up as a sealed, dust-tight containment vessel that prevents powder escape across all operational interfaces:
1. Continuous Precision-Sealed Enclosure Covers
- Heavy-Gauge Dust Cover Assemblies: The upper screening box is fitted with a rigid, heavy-gauge stainless steel cover plate designed to withstand internal air pressure surges without flexing or bowing.
- Precision Profile Gasketing: Continuous channels host food-grade silicone or EPDM sponge gaskets, establishing an airtight seal around the entire perimeter of the screen frame.
- Uniform Tension Clamping: Heavy-duty, quick-acting latches apply even compression force across the gasket surface, preventing seal degradation caused by long-term structural vibration.
2. Negative-Pressure Aspiration & Exhaust Venting
- Integrated Dust Extraction Outlets: The top enclosure cover features sanitary Tri-Clamp or flanged exhaust spouts designed to couple directly with central plant dust collection systems or localized HEPA exhaust units.
- Air Displacement Balancing: As bulk powder enters the inlet chute at high tonnage, displaced air and fine airborne dust are drawn safely through the exhaust port, creating a slight negative pressure inside the screening chamber that prevents dust from blowing out through inlet or discharge points.
3. Static-Dissipative Flexible Interfaces
- Dust-Tight Sleeve Couplings: Material inlets and outlets are equipped with food-grade, static-dissipative polyurethane or silicone flexible boots that connect seamlessly to upstream hoppers and downstream convey lines.
- Electrostatic Grounding Arrays: Braided copper grounding straps bridge all isolated screen components, safely dissipating static electricity charges generated by high-velocity powder friction.
Operational & Environmental Benefits
Deploying a fully enclosed, dust-tight Linear Vibrating Screen provides major plant-wide operational advantages:
- Extended Cleanroom HEPA & HVAC Filter Life: Capturing dust at the screening source reduces ambient airborne particulate loads, extending cleanroom air filter service life and lowering utility costs.
- Simplified Environmental Compliance: Helps facility managers maintain cleanroom particle count compliance under ISO 14644-1 standards and simplify HACCP environmental auditing.
- Enhanced Operator Comfort & Ergonomics: Eliminates localized powder clouds during high-tonnage runs, fostering a cleaner, safer, and healthier workplace environment for plant personnel.
Partner with Gaofu Machinery
At Gaofu Machinery, we design industrial powder processing solutions that balance high-volume productivity with strict environmental containment. Contact our technical engineering team today to learn how our dust-tight Linear Vibrating Screen can protect your cleanroom air quality and optimize your protein powder screening line.